Case Study
Food & Beverage Industries Products
Gentle, hygienic bulk handling for processors who can’t afford to compromise on product quality
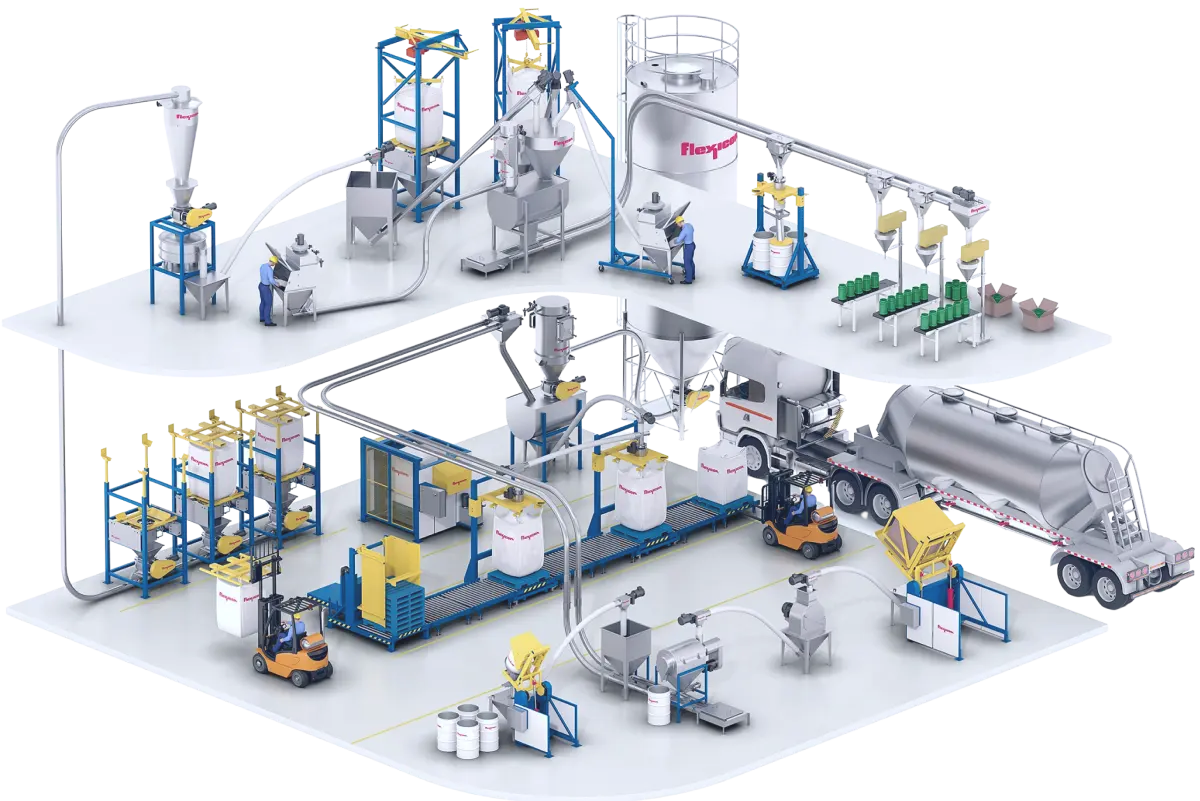
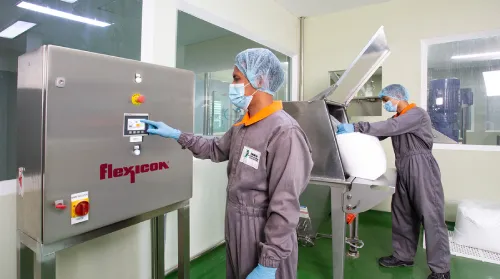
Food processing puts unusual demands on bulk material handling equipment. Products are often fragile, sticky, dusty, or prone to caking, and every system that touches them has to meet strict hygiene and food-safety standards while still keeping pace with high-volume production. Flexicon designs conveying, bulk bag handling, and weigh batching systems in food-grade stainless steel, built to move everything from delicate nuts and powdered ingredients to sugar, grain, and confectionery without damaging the product or compromising cleanliness.
For food and beverage processors across South Africa and the wider continent, this matters as much for compliance as it does for output. Equipment that gently handles friable ingredients, resists contamination, and washes down quickly between runs isn’t a nice-to-have — it’s what keeps a plant certified, efficient, and able to grow.
Featured Case Study
Almondco Boosts Almond Processing Output by Nearly 70% with a Custom Conveying and Storage System
Renmark, South Australia
The Challenge
Almondco, a leading almond processor established in 1944 and known for its high-quality “white box” brand, needed to significantly scale up its handling capacity as part of a major facility expansion. The new 10,000 m² processing and storage building was designed to consolidate operations and handle much larger volumes of raw and blanched almonds from its grower members. The catch: almonds are fragile. Any handling system had to move large quantities of nuts through multiple processing stages — pasteurising, blanching, slicing, packaging — without breaking or damaging them, while also keeping pace with production that was faster than the downstream equipment could absorb.
Flexicon’s Solution
Building on an existing relationship dating back to 2008, Almondco turned to Flexicon Australia to engineer the system. Flexicon specified six FLEXI-DISC® tubular cable conveyors, each custom-built for a specific run — different lengths, angles, and source-to-destination paths — to gently transport almonds through smooth stainless steel tubing using low-friction discs rather than aggressive mechanical handling. To absorb the mismatch between processing speed and downstream capacity, Flexicon also engineered a pair of large 12,500 kg stainless steel storage hoppers, feeding almonds down a spiral “let-down” chute that slows their descent and prevents damage. The entire six-conveyor system was integrated into a single plant-wide control system for seamless operation.
The Outcome
The completed system lifted Almondco’s processing output by nearly 70%, delivered within a seven-month build and installation window, and has run reliably since 2021. Locally manufactured equipment and readily available spare parts also meant Almondco could avoid the downtime risk of importing replacement components.
Additional Case Studies
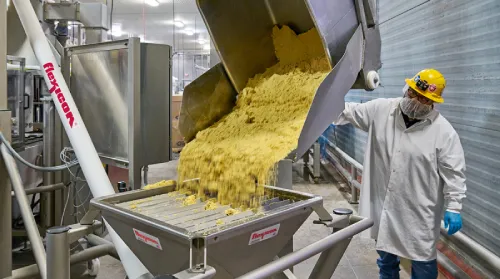
Lone Star Bakery Automates Dessert Production with Flexicon Screw Conveyor
A bakery replaced manual ingredient handling with a flexible screw conveyor to speed up and standardise dessert production.
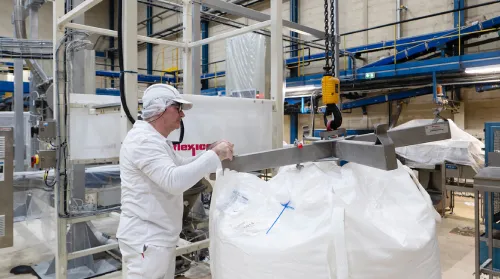
Sugar Fed from Bulk Bags Pneumatically at Tereos Artenay
Tereos Sucre uses a Flexicon pneumatic bulk handling system to move extra-fine sugar from bulk bags between production sites for cartoning and cube manufacture.
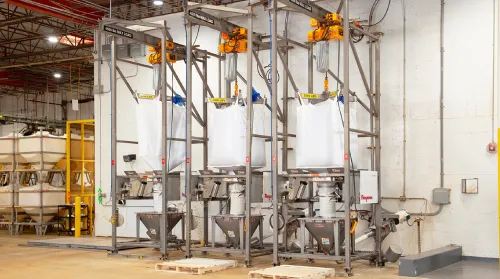
Automated Weigh Batching Increases Output, Ends Fatigue at Goya Florida
Sazon, Inc., a GOYA Foods manufacturing division, automated manual bag handling and batching of herbs, spices, and seasonings to cut fatigue and lift throughput.
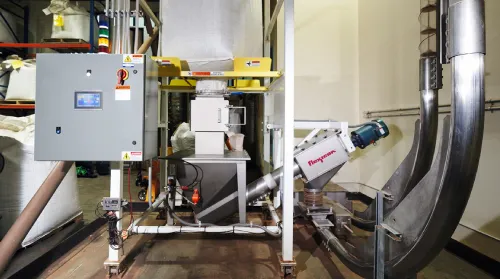
Bulk Handling System Triples Capacity, Cuts Staff by Two at Theo Chocolate
A craft chocolate maker scaled up production capacity threefold while reducing the labour needed for ingredient handling.
Distillery Loads Grain Nine Times Faster with Pneumatic Conveying Upgrade
Dancing Goat Distillery replaced a slow grain-loading process with a pneumatic conveying system, cutting load times dramatically.
Flexible Screw Conveying System Ups Production of Powdered Food Premix
Blaine Manufacturing Corporation increased output of its powdered food premix products with a flexible screw conveyor built for consistent, dust-controlled transfer.