Flexicon Product Range
Food & Beverage Industries
A product range built to move powders and bulk foods without breaking, contaminating, or slowing them down
Food processors ask more of their equipment than almost any other industry. Materials range from free-flowing sugar to oily, sticky spice blends and fragile roasted beans that can’t survive a rough conveyor. On top of that, every surface that touches product has to meet hygiene standards, resist wash-down, and keep dust — and the contamination and explosion risk that comes with it — out of the plant. Flexicon’s product range for Food Industries is engineered around exactly those constraints: gentle handling, dust-tight construction, and finishes built to food, dairy and pharmaceutical standards, in equipment that scales from a single stand-alone unit to a fully automated, plant-wide system.
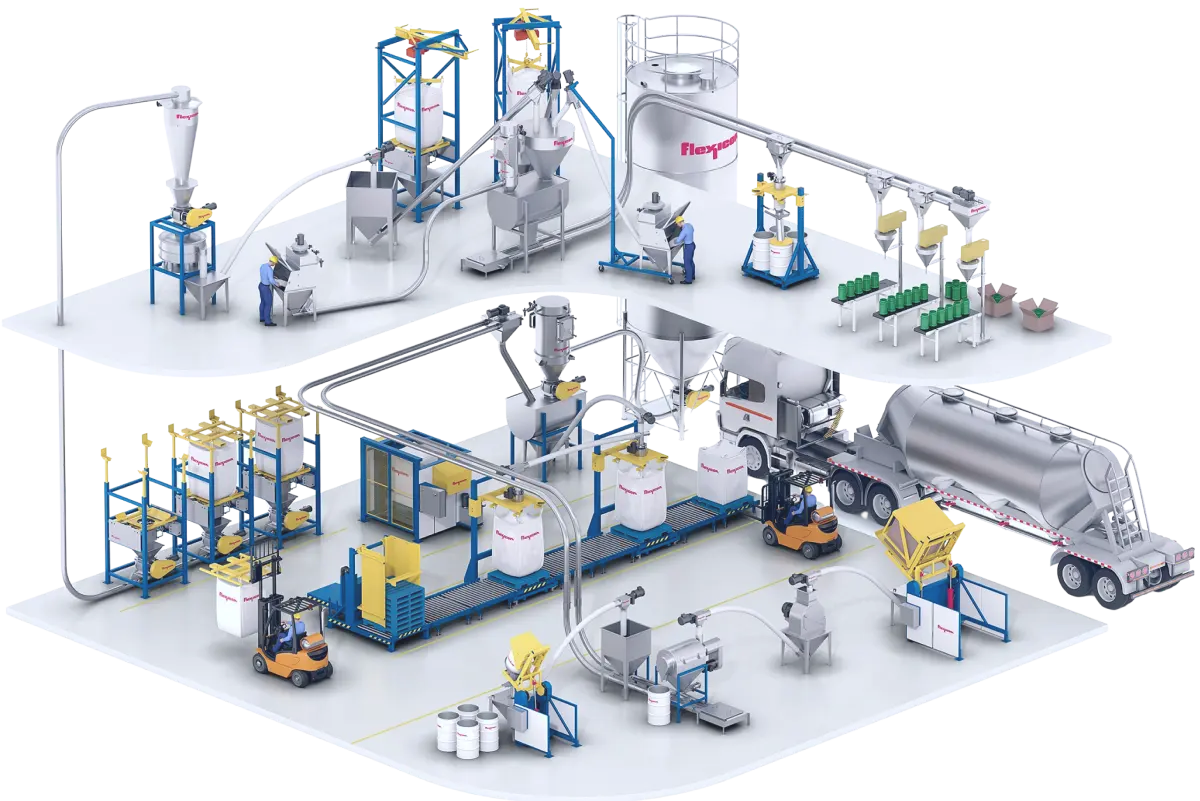
The Product Range
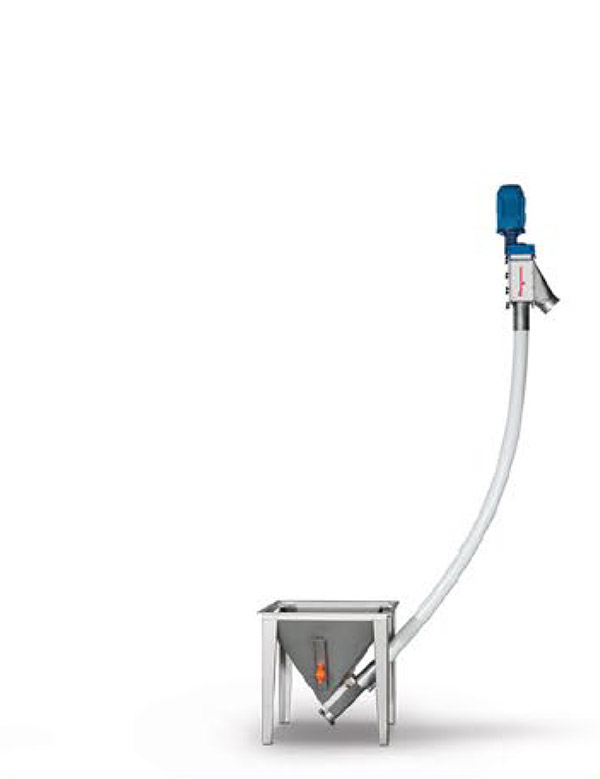
Flexible Screw Conveyors
Flexicon’s flexible screw conveyors move free- and non-free-flowing bulk foods — including products prone to packing, caking, smearing or fluidising — through a totally enclosed tube, with the motor positioned beyond the discharge point so material never contacts seals or bearings. That keeps moisture and temperature stable in transit and prevents blend separation, which matters for anything from milled spice to protein powder. Available in stainless steel finished to food, dairy or pharmaceutical standards.
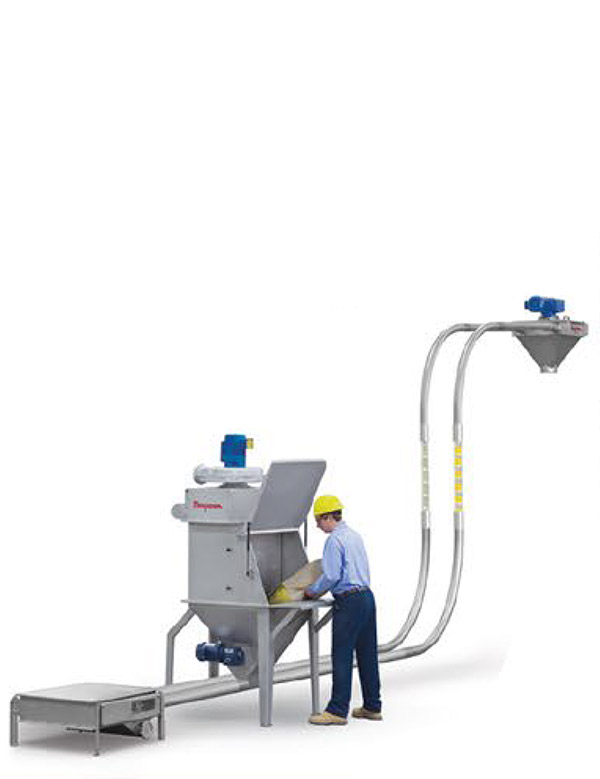
FLEXI-DISC® Tubular Cable Conveyors
For friable foods that can’t be conveyed the conventional way, Flexicon’s tubular cable conveyors slide material through smooth stainless steel tubing using low-friction polymer discs on a stainless cable. It’s a gentle, fully enclosed method suited to whole beans, nuts, dried fruit, cereals, snack pieces and frozen vegetables — anything that would chip, crack or degrade in a screw or belt conveyor. Routing can run horizontally, vertically or at any angle, through walls or ceilings, over short runs or hundreds of metres.
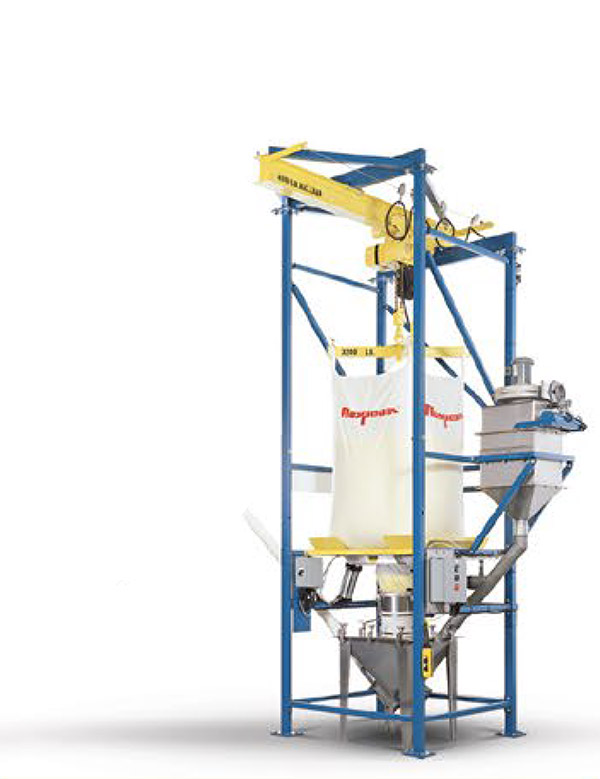
Bulk Bag Dischargers
BULK-OUT® bulk bag dischargers unload FIBCs into a process line dust-free, using a sealed bag-spout interface, flow-promotion devices, and full bag evacuation to reduce residual product waste. Frame options include forklift-loaded, hoist-and-trolley, and low-headroom half-frame models, all available in food-, dairy- or pharmaceutical-grade stainless steel.
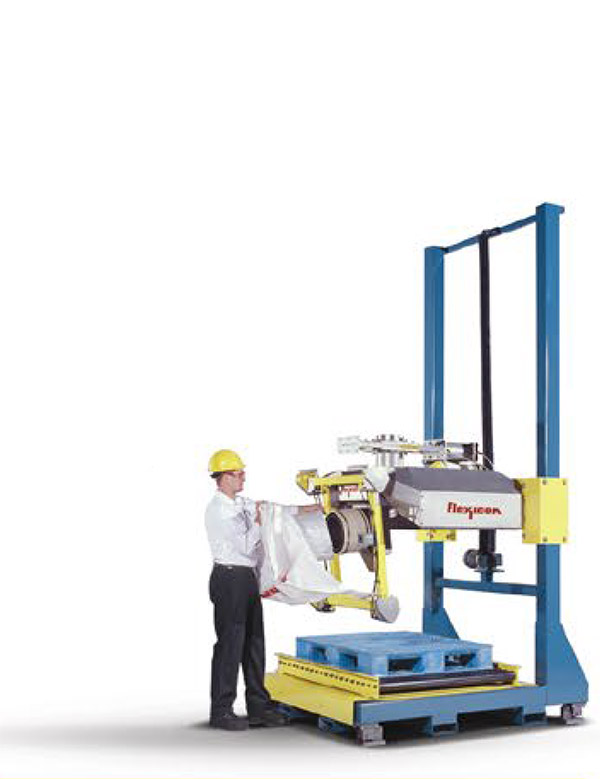
Bulk Bag Filling Systems
Sanitary bulk bag fillers weigh-fill and deaerate bulk bags automatically and dust-free, in all-stainless construction finished to sanitary standards — some models are USDA-accepted and 3-A/Dairy-standard compliant. Options include integral metal detection and separation, pivot-down fill heads that bring the connection point to floor level for the operator, and dual-filler configurations for rates up to 40 bags an hour.
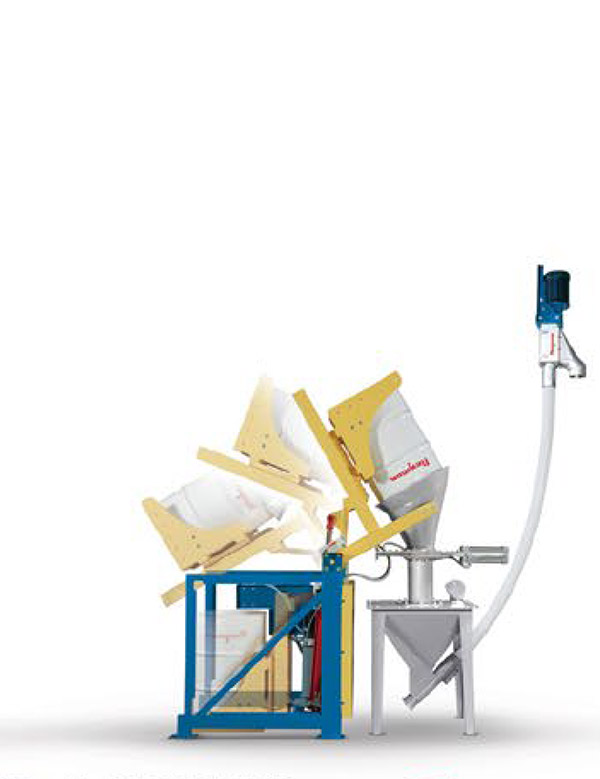
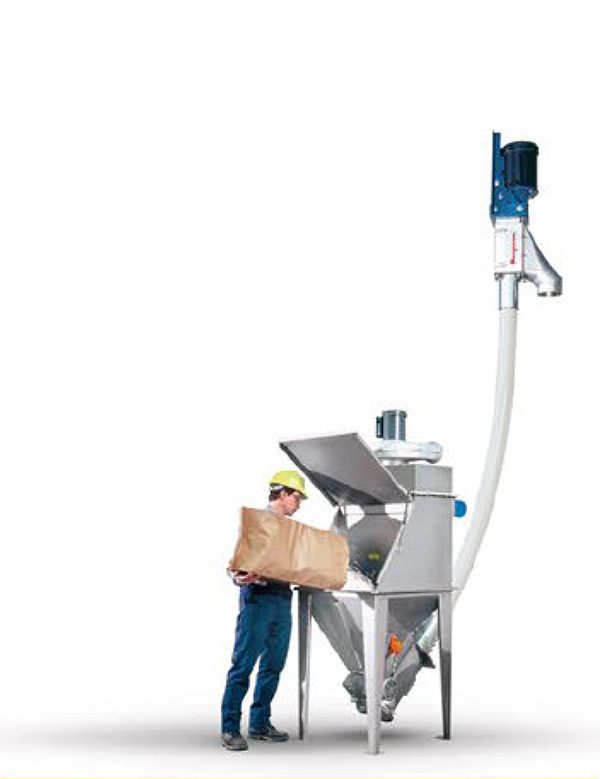
Bag Dump Stations
For hand-added ingredients, sack tip and bag dump stations capture dust at the point of manual dumping using a high-velocity vacuum fan and cartridge filters, returning captured product to the hopper instead of the plant atmosphere. Sanitary stainless models feature continuous welds and tool-free, rapid wash-down, and can be paired with a glove box for contamination-sensitive or allergen-controlled materials.
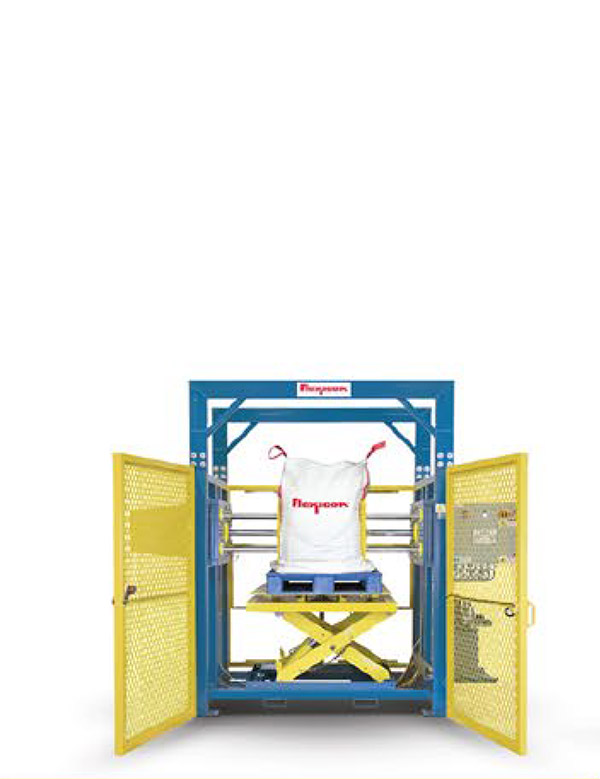
Bulk Bag Conditioners
Food ingredients that solidify in storage — sugar, salt, milk powder, spice blends — often can’t be freed by a discharger’s built-in flow aids alone. Flexicon’s sanitary bulk bag conditioner uses contoured hydraulic rams to press and loosen the bag from multiple sides and heights before discharging, restoring flow without opening the bag or exposing the product.
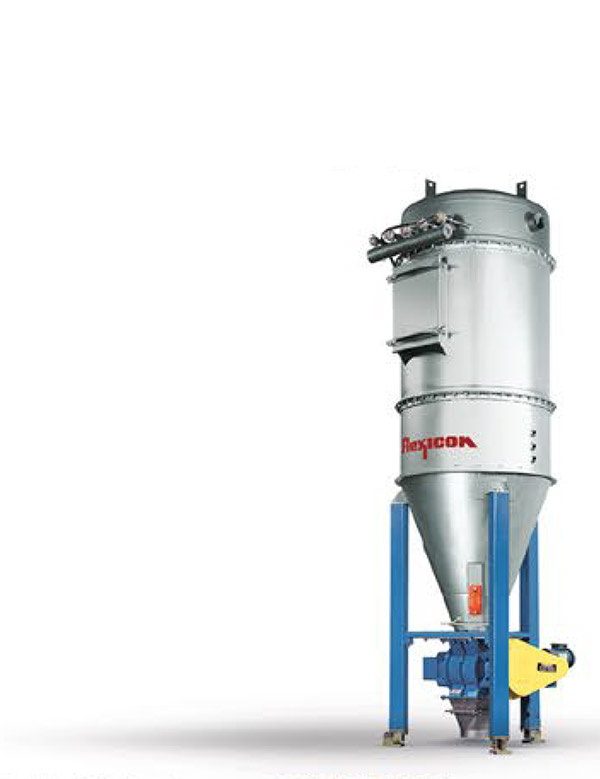
Pneumatic Conveying Systems (PNEUMATI-CON®)
Dilute-phase vacuum and positive-pressure pneumatic systems move powders, granules and friable foods fully enclosed over long distances and complex routing, minimising floor space and cross-contamination between ingredients. Built in stainless steel to food, dairy or pharmaceutical finish, with gain-in-weight hoppers available for accurate batch delivery downstream.
Weigh Batching Systems
For multi-ingredient recipes, Flexicon’s automated weigh batching systems combine major and minor ingredient feeds — up to seven major components and unlimited minor ones on a single system — into precise, repeatable batches. Enclosed material paths keep dust and cross-contamination down, which matters as much for hygiene compliance as for recipe accuracy.
Drum, Box & Container Dumpers
TIP-TITE® dumpers form a dust-tight seal to drums, boxes and other containers, then tip and discharge bulk material at a controlled rate — a sanitary option for handling ingredients that arrive in rigid containers rather than bags.
Proven in the Field
Bulk Handling That Protects Product Quality, Not Just Throughput
Food processing asks something most industries don’t: move product fast, at volume, without damaging it. Delicate ingredients bruise or break under aggressive handling. Sticky, dusty, or caking products clog equipment not designed with them in mind. And every system touching the product has to satisfy hygiene and food-safety standards that don’t bend for the sake of output.
Flexicon Africa designs conveying, bulk bag handling, and weigh batching systems in food-grade stainless steel, built to move fragile and friable products — nuts, powdered ingredients, sugar, grain, confectionery — gently enough to protect yield, while still keeping pace with high-volume production and washdown requirements between runs.
The case studies below show how Flexicon’s engineering has solved these same challenges for food and beverage processors worldwide — from lifting almond processing output by nearly 70% to ending manual batching fatigue — insight now available to South African processors, backed by local support out of Gqeberha.