Flexicon Product Range
Industrial Chemicals
A versatile product range designed to handle challenging materials, including abrasive, dusty, flammable and hazardous substances.
Industrial chemical powders push equipment to its limits. Some abrade metal on contact. Some throw fine, explosive dust into the air. Some are corrosive or toxic enough that a leaking seal is a safety incident, not just a housekeeping problem. Others absorb moisture from the air and set solid in storage. Flexicon’s product range for Industrial Chemicals is built around exactly those constraints: fully enclosed, dust-tight construction, wear-resistant materials of construction, and containment designed to keep operators safe and product where it belongs — in the process, not the plant atmosphere.
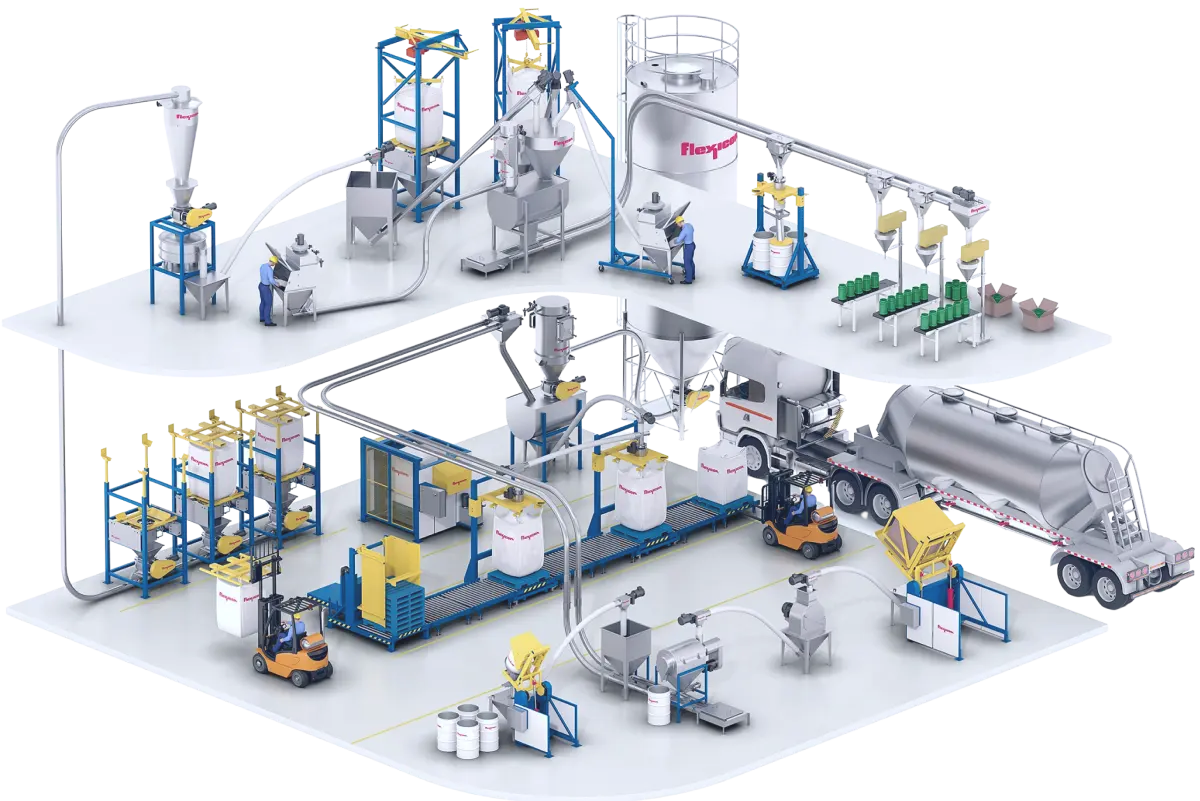
The Product Range
Flexible Screw Conveyors
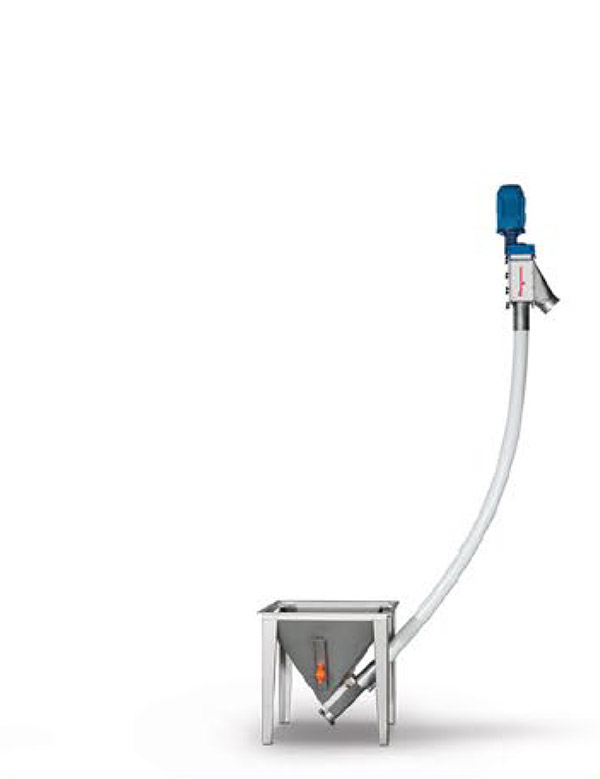
Flexicon’s flexible screw conveyors move abrasive, dusty and hygroscopic chemical powders through a totally enclosed, spiral-driven tube. Because the drive motor sits beyond the discharge point, material never contacts seals, bearings or open shafts — reducing wear points and eliminating a common source of contamination and leak-related exposure. Suitable for everything from free-flowing salts to sticky, packing powders like calcium stearate or fumed silica.
Pneumatic Conveyors
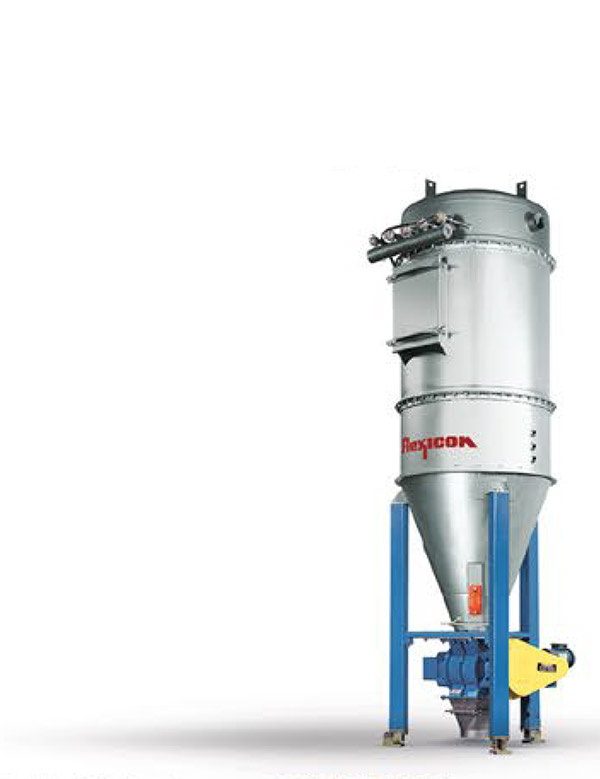
For chemical operations that need to move product through long or routed pipeline runs — or keep it fully sealed from ignition sources — Flexicon’s dilute-phase, dense-phase and vacuum pneumatic conveyors transport material using air or inert gas rather than mechanical contact. This makes them well suited to flammable and hazardous powders where dust generation and static ignition risk have to be tightly controlled, and to installations where product must cross multiple floors or building sections.
Bulk Bag Dischargers
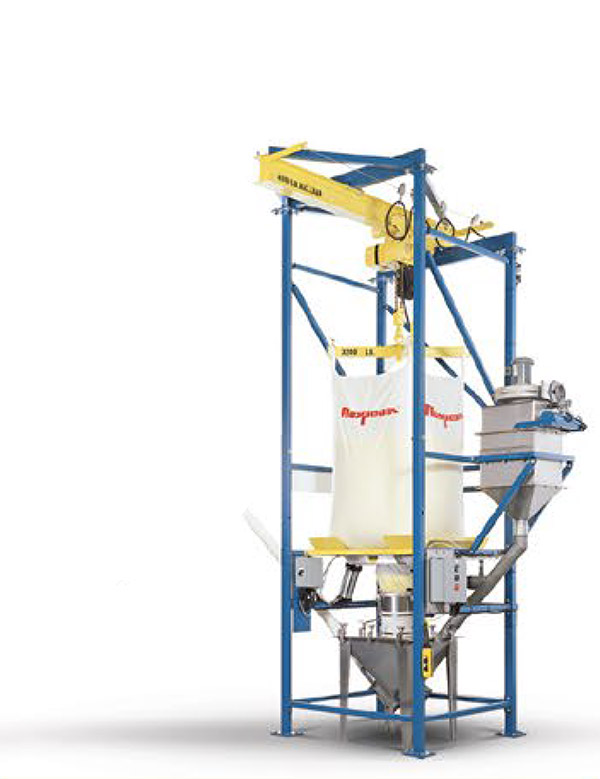
BULK-OUT® bulk bag dischargers unload FIBCs of chemical powders dust-free, using a sealed bag-spout interface, flow-promotion devices and full bag evacuation. For abrasive or corrosive materials, wear-resistant liners and chemical-duty finishes extend service life; for hazardous or toxic powders, containment features keep the operator out of the dust path entirely.
Bulk Bag Filling Systems
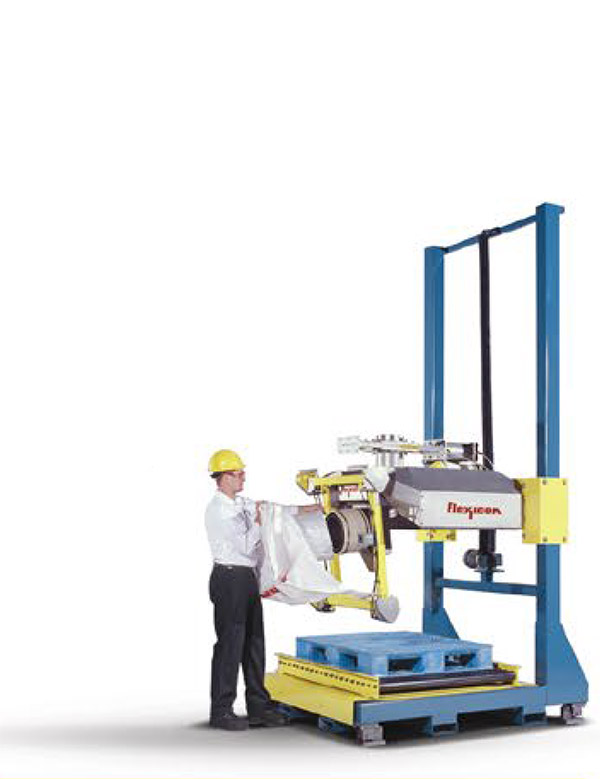
Automated bulk bag fillers weigh, fill and deaerate chemical powders into FIBCs with minimal dust escape — a critical requirement for fine, dense materials like alumina oxide or titanium dioxide that entrain air and resist settling. Deaeration and densification features prevent bags from being under-filled or unstable in transit, addressing a common bottleneck in chemical bagging lines.
BLOCK-BUSTER® Bulk Bag Conditioners
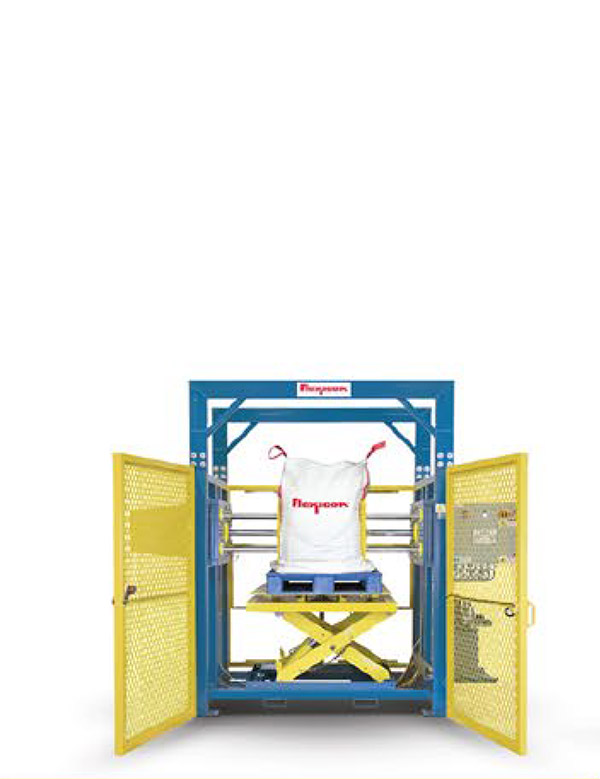
Hygroscopic chemicals — resins, hydrates, salts and similar materials — absorb moisture during storage and shipment and solidify into unusable lumps. Flexicon’s hydraulic bulk bag conditioners knead the bag from the outside to break up caked material and return it to a free-flowing state before it reaches a discharger, without opening the bag or exposing operators to the product.
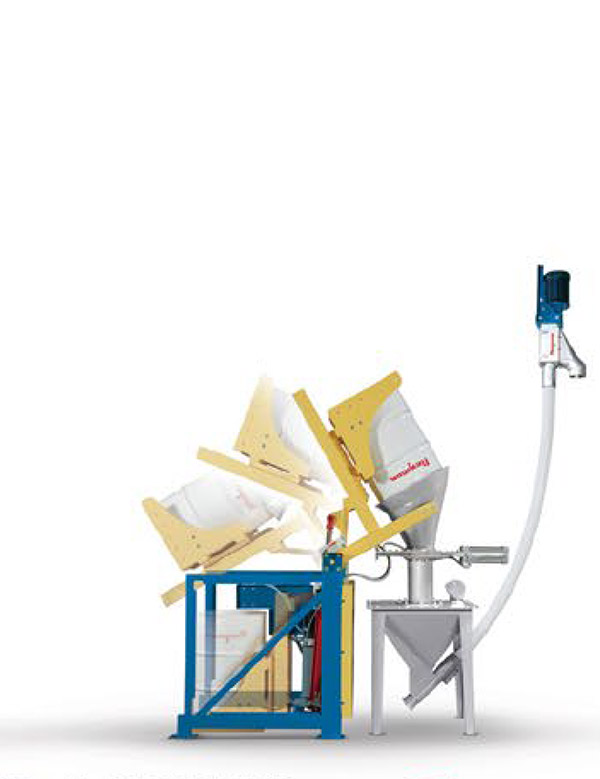
Bag Dump Stations
For hand-added or smaller-volume chemical ingredients, sack tip and bag dump stations capture dust at the point of manual dumping using a high-velocity extraction fan and cartridge filters, returning reclaimed product to the process instead of releasing it into the plant — reducing both product loss and operator exposure to fine or hazardous dust.
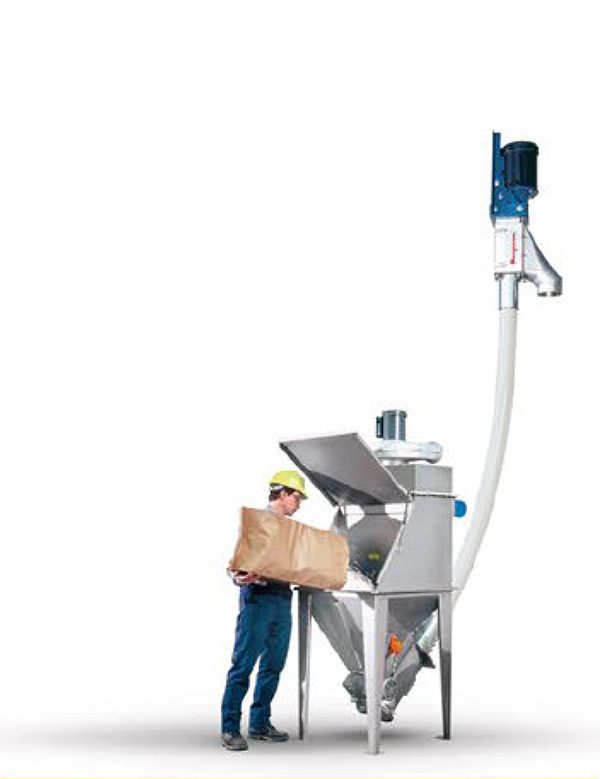
Drum, Box & Container Dumpers
Where chemicals arrive in drums, boxes or other rigid containers rather than bags, Flexicon’s dumpers invert and discharge the container into a hopper or receiving vessel under dust containment, cutting out the manual lifting and open-pour handling that create both safety and contamination risk.
Weigh Batching Systems
For chemical processes that combine multiple ingredients to precise formulations, Flexicon’s weigh batching systems automate the metering, weighing and blending of powders from various feed sources, improving batch accuracy and repeatability while reducing manual handling of hazardous or high-value materials.
Automation & Controls
Every component in the range can be tied together under a single control platform — sequencing fill and discharge cycles, monitoring dust collection, and logging batch data — so the equipment scales from a single stand-alone unit to a fully automated, plant-wide chemical handling system.
Proven in the Field
Bulk Handling Built for Chemical Manufacturing’s Toughest Materials
Chemical processing carries little tolerance for equipment that isn’t matched to the material. Hygroscopic powders clump in storage and jam a line before a shift even gets going. Fine dusts raise real combustion risk. Resins and acids wear through conveying components never designed to hold up against them. In an industry where batch accuracy and worker safety are non-negotiable, the equipment moving your raw materials is part of the process control itself, not an afterthought to it.
Flexicon Africa designs bulk bag handling, flexible screw conveying, and pneumatic conveying systems around exactly these demands — built to keep hazardous, agglomerating, or abrasive materials moving safely and accurately, with the containment and hazardous-area compliance South African chemical manufacturers are increasingly required to meet.
The case studies below show how Flexicon’s engineering has solved these same problems for chemical processors around the world — from de-lumping resin ingredients to enclosing combustible powders — backed by local support out of South Africa.