Case Study
Pharmaceutical & Nutraceutical Products
Bulk material handling built for South Africa’s booming supplement and pharma sector
Pharmaceutical and nutraceutical powders are some of the least forgiving materials in bulk handling — fine, dust-prone, often hygroscopic, and always contamination-sensitive. A single cross-contamination event or dusting incident can mean a failed batch, a regulatory finding, or a health and safety liability. Flexicon designs conveying, bulk bag handling, and dust-containment systems engineered to move these materials cleanly, accurately, and in full compliance with GMP standards.
With South Africa’s sports nutrition and supplement manufacturing sector expanding rapidly — much of it, under local regulation, held to the same standards as pharmaceutical products — reliable, locally built bulk handling has become a competitive necessity, not a nice-to-have. Flexicon has engineered and manufactured its full equipment range from Gqeberha since 1999, giving South African pharmaceutical and nutraceutical producers local access to a company with more than 25,000 installations worldwide.
Featured Case Study
Globepak scales up to 360+ sports nutrition products across seven automated lines
Centurion, South Africa
Globepak (Pty) Ltd, a wholly-owned subsidiary of the USN Group, manufactures one of the largest ranges of powdered sports nutrition and supplement products on the continent — everything from whey protein and plant-based proteins to creatine and amino acid blends. As demand for sports nutrition surged across South Africa and export markets, Globepak’s original 4,000 m² facility became the bottleneck: its rigid intermediate bulk containers (IBCs) and fixed auger conveyors simply couldn’t feed the plant’s blenders and packaging lines fast enough. “They were starving the packaging lines,” as the engineering firm brought in to fix the problem put it.
The Challenge
Globepak needed a new, much larger facility that could handle a huge diversity of powder characteristics — sticky, free-flowing, fine and dusty, sometimes all in the same shift — without cross-contaminating between the 360+ different products running through the plant. Whatever system replaced the old IBCs also had to meet Good Manufacturing Practice standards, since South African regulation treats nutritional supplements as pharmaceutical products.
The Solution
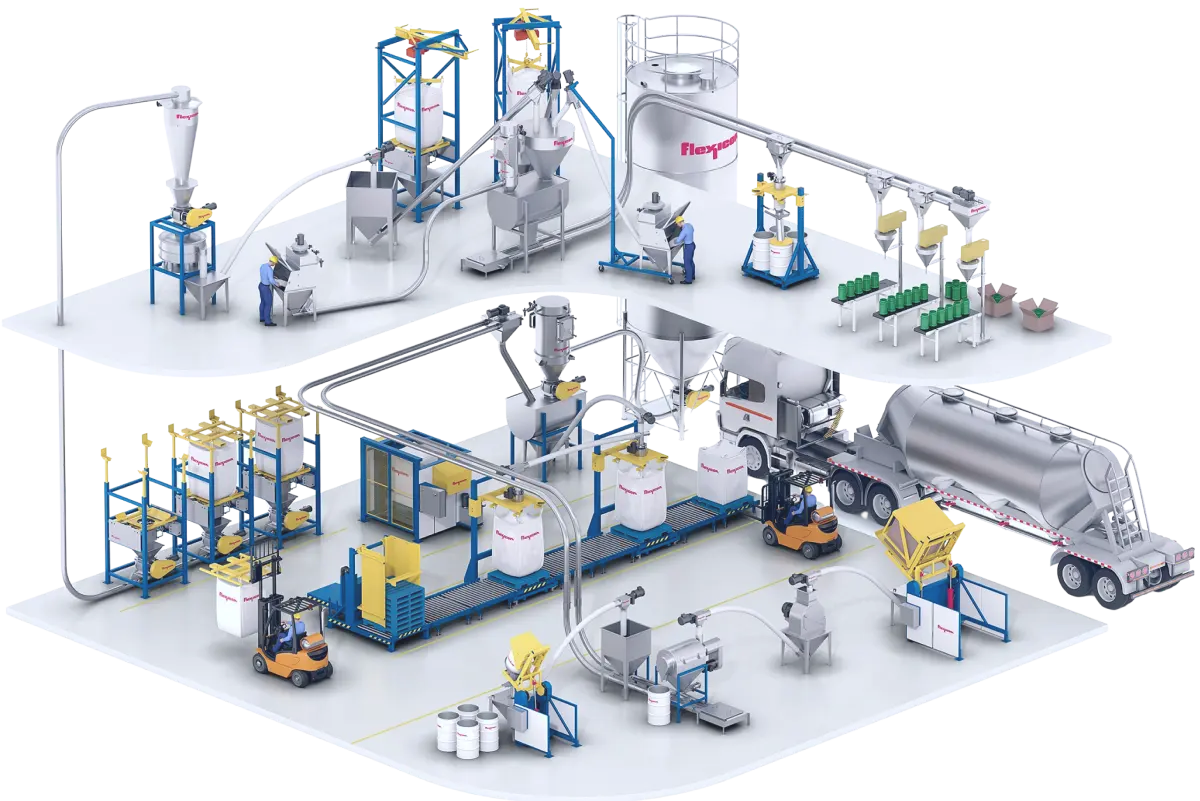
Working with local systems integrator DC Weighing and Control, Flexicon Africa supplied seven identical automated bulk handling lines for Globepak’s new 14,000 m² Centurion plant, completed in 2021. Each line pairs a Flexicon BFC BULK-OUT® bulk bag discharger with a flexible screw conveyor to move ingredients from bulk bag to packaging machine under full PLC control. Operators load bags without a forklift, using a cantilevered hoist and pendant control, and connect each bag through a sealed spout interface that keeps material fully enclosed from the moment the bag opens to the moment it reaches the packaging hopper — a genuine “no-touch” process. Level sensors on each packaging line automatically start and stop the conveyors to keep production continuous, and a full product changeover — including cleaning — takes around 15 minutes.
The Outcome
The new system gave Globepak the throughput, hygiene, and flexibility to keep pace with soaring demand while meeting the sanitary standards its regulatory status demands. Changeovers between flavours and formulations now take minutes rather than hours, dust and cross-contamination risks have been effectively eliminated, and the plant has capacity in reserve as USN eyes expansion into European, UK, and US markets, along with a planned facility in Kenya to serve central and west Africa.
Additional Case Studies
Epic Pharma
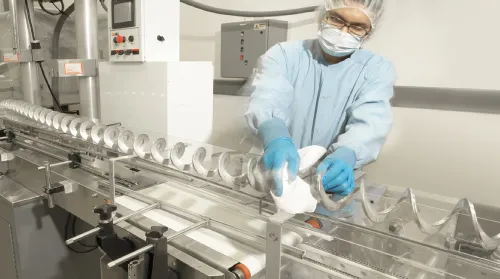
A US generic pharmaceutical manufacturer replaced manual drum-lifting and hand-scooping of a fine, hygroscopic resin with automated flexible screw conveyors, eliminating dusting and spillage on its packaging line.
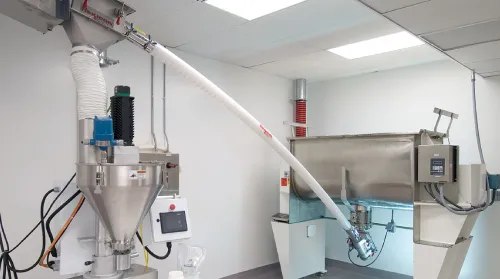
Macleod Pharmaceuticals
Tight space constraints and strict anti-contamination requirements for powdered antibiotics led this manufacturer to a curved flexible screw conveyor that fit between blender and filler while keeping the product completely dust-tight.
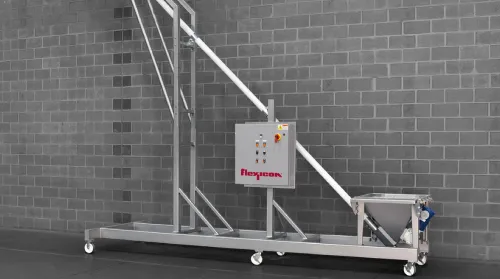
SMK Nutra Makers
A US dietary supplement and nutritional product formulator replaced a laborious, dusty process of hand-dumping powder from an elevated safety cage with mobile flexible screw conveyors, improving both throughput and operator safety.
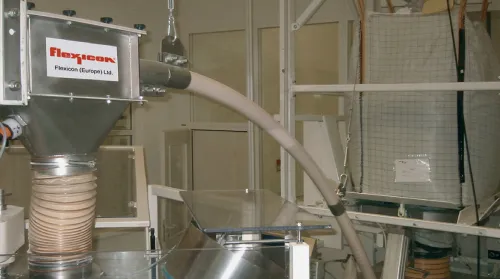
Orthomol
To meet HACCP and other international certification requirements, this nutritional products manufacturer moved from manual bag dumping to a fully enclosed bulk bag unloading and conveying system that prevents moisture-sensitive granules from agglomerating or separating.